English
 Français
 Español
 русский
 عربى
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Green Ohm
Content
- 1 1. The Role of LSZH Sheathing in Modern Power Networks
- 2 2. Product Positioning and Application Scope
- 3 3. Key Performance Advantages
- 3.1 3.1 Low-Smoke Combustion Behavior
- 3.2 3.2 Halogen-Free and Low-Corrosivity Characteristics
- 3.3 3.3 Flame Retardancy and Oxygen Index
- 3.4 3.4 Mechanical Strength and Elongation
- 3.5 3.5 Heat Aging Stability
- 3.6 3.6 Resistance to Hot Deformation
- 3.7 3.7 Low-Temperature Performance
- 3.8 3.8 Electrical Insulation Performance
- 3.9 3.9 Heat Shock and Ozone Resistance
- 4 4. Typical Technical Data
- 5 5. Advantages Over Conventional and Lower-Specification Alternatives
- 6 6. Advanced Manufacturing and Research Strengths
- 7 7. Manufacturing Process Considerations for Cable Producers
- 8 8. Application Areas
- 9 9. Selecting Between the Available Grades
- 10 10. Environmental and Regulatory Considerations
- 11 11. Quality Assurance and Customer Service
- 12 12. Recommended Evaluation Procedure
- 13 13. Frequently Asked Questions
- 13.1 What is an LSZH cable sheathing compound?
- 13.2 What is the main application of this product?
- 13.3 What is the difference between the B1 and B2 grades?
- 13.4 Are the materials halogen-free?
- 13.5 Do these compounds generate low smoke?
- 13.6 Can the material be used outdoors?
- 13.7 Can the material be used for buried cables?
- 13.8 What is the tensile strength of the material?
- 13.9 What is the elongation at break?
- 13.10 Does the material resist heat?
- 13.11 Is the material suitable for low-temperature installation?
- 13.12 What electrical insulation performance is reported?
- 13.13 Is the material thermoplastic or cross-linked?
- 13.14 Can the grades be customized?
- 13.15 What support can a cable manufacturer expect?
- 14 14. Conclusion
- 15 References
- 16 Product: LSZH Flame Retardant Sheathing Material for Power Grids (Class B1/B2)
Power transmission and distribution networks require cable materials that can perform reliably under electrical, mechanical, thermal, environmental, and fire-related stresses. The outer sheath is the first protective barrier between the cable core and its surroundings. It must resist abrasion, moisture, ultraviolet exposure, temperature changes, cracking, and chemical attack while also limiting the spread of fire and reducing the production of smoke and corrosive gases. These requirements become especially important in substations, switchgear rooms, underground distribution systems, public infrastructure, industrial facilities, transport networks, and densely occupied buildings.
Thermoplastic low-smoke zero-halogen, or LSZH, sheathing compounds are designed to address these challenges. The LSZH flame-retardant sheathing material described in this article is developed for power grid transmission and distribution cables and is available in standard grades identified as DS-WDZH-01, DS-WDZH-02, DS-WDZH-03, DS-WDZH-B1, and DS-WDZH-B2. The material combines low smoke generation, halogen-free combustion behavior, flame retardancy, electrical insulation, outdoor durability, and resistance to cracking.
Its main value is not limited to passing an individual flame test. A cable sheath must provide balanced performance across many requirements. Excessive flame-retardant additives can reduce flexibility or mechanical strength. A formulation that performs well in a laboratory flame test may become brittle at low temperature, deform under heat, or lose durability in outdoor conditions. The material described here is engineered as a balanced compound for practical cable production, helping cable manufacturers address fire safety and long-term service requirements through one integrated sheathing solution.
1. The Role of LSZH Sheathing in Modern Power Networks
Power cables operate in environments where failure can have serious consequences. A cable may be installed in a buried conduit, laid directly underground, routed through a cable tunnel, mounted on an outdoor structure, placed near switchgear, or installed in a facility containing sensitive electrical equipment and people. In each case, the sheath must protect the insulation system while limiting the consequences of an incident.
Traditional halogen-containing materials can release acidic and corrosive gases when exposed to fire. These gases may damage metallic equipment, electronic components, connectors, and structural elements. Dense smoke can also reduce visibility, complicate evacuation, and make firefighting more difficult. LSZH compounds are formulated without intentionally added halogen-based flame-retardant systems and are designed to produce limited smoke and low levels of halogen acid gas during combustion.
The importance of these characteristics is particularly clear in enclosed or semi-enclosed areas. Underground cable galleries, substations, utility tunnels, commercial buildings, data centers, factories, transportation facilities, and control rooms may contain a high concentration of cables. If a fire occurs, the sheath should not become a major source of flame spread, dense smoke, or corrosive emissions.
At the same time, power cable sheathing cannot be treated solely as a fire-safety component. The material must also maintain tensile strength, elongation, insulation resistance, and dimensional stability. It must tolerate installation forces, thermal cycling, environmental exposure, and the normal movement of cables during service. The performance data supplied for these grades reflect this multi-factor approach.
2. Product Positioning and Application Scope
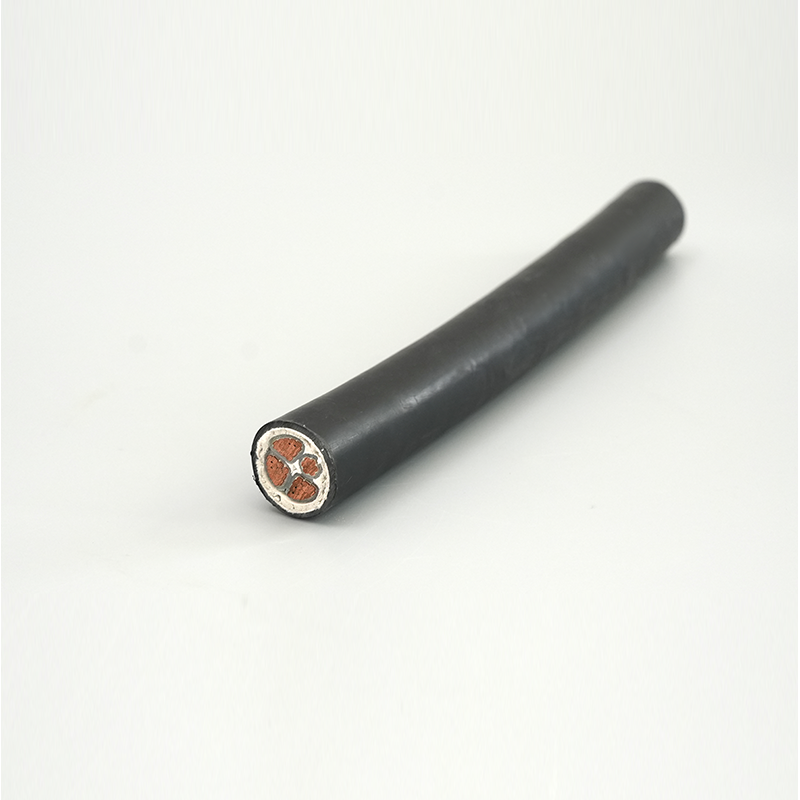
The product is a thermoplastic LSZH sheathing compound for power grid cables. It is intended for the outer protection of transmission and distribution cables, including overhead cable-related applications, buried distribution cables, and switchgear wires. The compound can also be considered for other cable constructions where low smoke, halogen-free behavior, flame retardancy, outdoor durability, and electrical insulation are required.
The available grades cover general-purpose LSZH performance and higher flame-retardant levels designated B1 and B2. The grade selection should be made according to the cable design, extrusion process, required fire classification, installation environment, and the applicable project specification. The material supplier or cable manufacturer should confirm the appropriate grade through production trials and final cable testing.
Although the material is thermoplastic, the listed performance note indicates that the stated performance indicators are measured after cross-linking. This point is important for engineering evaluation. Processing conditions, cross-linking method, cable construction, wall thickness, cooling conditions, and test specimen preparation can all influence final results. The compound should therefore be evaluated not only as a raw pellet but also as part of the finished cable system.
The product’s application value comes from its combination of properties:
• Low smoke generation in both flaming and non-flaming conditions.
• Halogen acid gas content below the stated standard limit.
• Combustion pH and conductivity values that indicate low corrosive potential.
• Oxygen index values from at least 30 percent for the listed grades, with higher typical values for the B1 and B2 grades.
• Strong tensile properties and elongation suitable for cable sheathing.
• Low hot deformation at 90 degrees Celsius.
• Resistance to cracking during heat shock and ozone exposure.
• Stable electrical insulation performance, including volume resistivity above 1012 ohm-centimeters.
• Resistance to low-temperature embrittlement at the specified impact temperature.
• Compatibility with outdoor, buried, and switchgear-related cable uses.
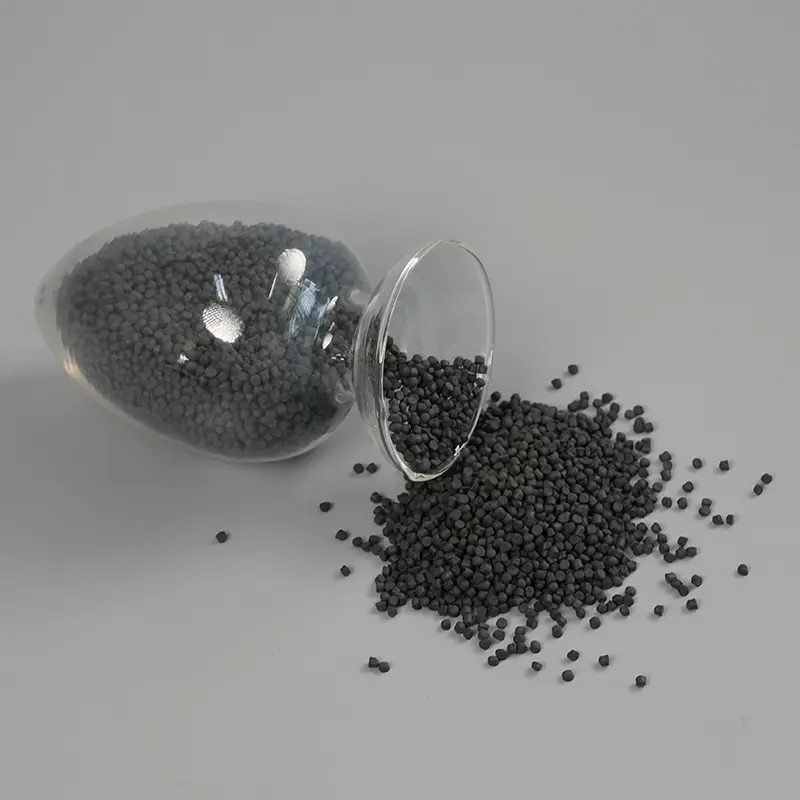
LSZH Flame Retardant Sheathing Material for Power Grids (Class B1/B2)
3. Key Performance Advantages
3.1 Low-Smoke Combustion Behavior
Smoke density is a critical factor in the safety performance of cable materials. During a fire, smoke can impair visibility before flames directly affect personnel or equipment. The reported smoke-density values for the standard grades are 305, 320, and 340 under non-flaming conditions, while the B1 and B2 grades show typical values of 260 and 280. Under flaming conditions, the reported values range from 50 to 70, compared with the stated standard limit of 100.
These results show that the B1 and B2 grades provide particularly favorable smoke performance in the supplied data. Lower smoke generation can support emergency response, evacuation, inspection, and post-fire recovery. It may also reduce the amount of smoke deposited on nearby electrical equipment and building surfaces.
Compared with conventional flame-retardant cable materials that may release large amounts of dense smoke, the LSZH formulation is designed to reduce the visual and corrosive burden associated with cable combustion. This is a significant advantage in installations where cables pass through occupied buildings, enclosed technical spaces, or areas containing expensive electrical and electronic equipment.
3.2 Halogen-Free and Low-Corrosivity Characteristics
The halogen acid gas content for all listed grades is reported as less than 0.5 percent, meeting the stated requirement of no more than 0.5 percent. The pH values range from 5.1 to 5.5, above the specified minimum of 4.3. Conductivity values range from 1.1 to 1.2 microsiemens per millimeter, substantially below the stated maximum of 10 microsiemens per millimeter.
These measurements are relevant because combustion gases can become corrosive when they contain acidic compounds. A material that produces less acidic and less conductive combustion residue may help reduce secondary damage to metal, electrical contacts, circuit boards, control equipment, and other components located near the cable route.
The halogen-free design also aligns with the growing demand for safer cable systems in public infrastructure and environmentally sensitive projects. It is important to distinguish this product characteristic from a general claim that no combustion products are harmful under all conditions. Any cable fire requires professional safety management. However, the reported acid gas, pH, and conductivity results demonstrate that the material is designed to limit key corrosive combustion indicators.
3.3 Flame Retardancy and Oxygen Index
The oxygen index indicates the minimum oxygen concentration required to support combustion under a specified test method. The listed standard requires an oxygen index of at least 30 percent. Typical values are reported as at least 35 percent for DS-WDZH-01, at least 32 percent for DS-WDZH-02, at least 30 percent for DS-WDZH-03, at least 40 percent for DS-WDZH-B1, and at least 38 percent for DS-WDZH-B2.
The higher typical oxygen-index values of the B1 and B2 grades indicate enhanced resistance to sustained combustion in the stated test conditions. This makes them suitable candidates for cable applications where a higher flame-retardant requirement is specified. The final fire classification, however, depends on the complete cable, its construction, the amount of material used, installation conditions, and the relevant test standard.
A major advantage of a purpose-designed LSZH formulation is the ability to combine flame retardancy with mechanical and electrical properties. Some heavily filled flame-retardant systems can become difficult to process or may show reduced elongation. The reported values for these materials demonstrate that the formulation is designed to preserve a practical balance between flame performance and sheath integrity.
3.4 Mechanical Strength and Elongation
Tensile strength is an important indicator of a sheath’s ability to withstand pulling, handling, and mechanical stress. The stated standard is 10.0 MPa, while the typical values range from 11.2 to 12.5 MPa. The DS-WDZH-03 grade shows the highest listed typical tensile strength at 12.5 MPa, while the B1 and B2 grades each show a typical value of 11.2 MPa.
Elongation at break is reported at 160 percent or higher under the standard, with typical values of 170 or 180 percent for the listed grades. Adequate elongation helps the sheath tolerate bending, installation movement, thermal expansion, and local stress concentration without premature rupture.
When compared with compounds that focus narrowly on flame performance, these tensile and elongation values are a practical competitive advantage. A cable sheath must remain intact not only during a fire test but also during manufacturing, transportation, installation, and years of service. Mechanical balance can reduce the risk of cracks, tears, and damage caused by pulling or bending.
3.5 Heat Aging Stability
The heat-aging test is carried out at 110 degrees Celsius for 168 hours. The stated requirements allow tensile-strength and elongation change rates within plus or minus 25 percent. The typical tensile-strength change rates range from plus 9 to plus 14 percent, while the elongation change rates range from minus 5 to minus 15 percent.
These results indicate that the material retains a substantial portion of its original mechanical performance after accelerated heat exposure. Controlled change rates are important for cables installed near power equipment, in warm technical areas, in cable trenches, or in environments where daily and seasonal temperatures fluctuate.
Good heat-aging behavior also supports manufacturing consistency. A cable compound that changes excessively during service may become harder, weaker, or more prone to cracking. The reported data suggest that the formulation has been developed to maintain stable sheath behavior over time rather than providing only short-term flame-retardant performance.
3.6 Resistance to Hot Deformation
Hot deformation is tested at 90 degrees Celsius for one hour. The specified limit is no more than 50 percent. The reported typical values are between 5 and 10 percent, which provides a substantial margin relative to the listed requirement.
Low hot deformation helps the sheath maintain its shape and thickness when exposed to elevated temperatures. This is valuable for cables carrying current, cables installed in warm environments, and cable systems where dimensional stability affects mechanical protection or electrical spacing.
For cable manufacturers, good hot deformation performance may also support more consistent extrusion dimensions. A stable sheath can help maintain product geometry during cooling and subsequent handling. Final results will depend on extrusion temperature, line speed, die design, cooling conditions, and cable construction, but the compound’s typical test results provide a strong starting point for process development.
3.7 Low-Temperature Performance
The embrittlement temperature by impact is listed as minus 25 degrees Celsius for all five material grades. This indicates that the material is designed to resist impact-related embrittlement at the specified low temperature.
Low-temperature performance is important for outdoor cables, seasonal installation work, cold storage areas, northern climates, and transportation or construction sites where cable products may be handled before the ambient temperature has risen. A sheath that becomes brittle during cold installation may crack under impact, bending, or pulling.
The low-temperature result complements the heat-resistance data. Together, the results show that the material is intended to operate across a relatively broad temperature range. Engineers should still confirm the complete cable’s minimum installation and operating temperature according to the cable design and relevant standards.
3.8 Electrical Insulation Performance
Volume resistivity at 20 degrees Celsius is specified as at least 1012 ohm-centimeters. The typical values are 1.2×10¹³ to 2.5×10¹³ ohm-centimeters. The B1 and B2 grades show typical values of 2.5×10¹³ ohm-centimeters.
High volume resistivity supports the sheath’s role as an electrically insulating protective layer. Although the sheath is not always the primary insulation around the conductor, its electrical properties contribute to the overall safety and reliability of the cable system. Stable resistivity can be especially important in damp or outdoor environments where surface contamination and moisture may otherwise increase electrical risk.
The reported resistivity results are also useful when comparing LSZH products. Some flame-retardant systems may show reduced electrical performance because of their filler package or moisture sensitivity. The values provided here indicate that the formulation is designed to preserve a high level of electrical insulation while incorporating flame-retardant and low-smoke features.
3.9 Heat Shock and Ozone Resistance
In the heat-resistance-to-shock test at 130 degrees Celsius for one hour, all listed grades show no cracking. The ozone resistance test, conducted at 25 degrees Celsius for 24 hours at 300 parts per million, also shows no cracking for every grade.
Crack resistance is essential because even a small sheath crack can provide a pathway for moisture and contaminants. Over time, cracking may reduce mechanical protection and expose underlying layers to environmental stress. Resistance to thermal shock and ozone is therefore directly related to long-term cable durability.
Ozone resistance is particularly relevant to outdoor installations and locations near electrical equipment where ozone may be generated. The no-cracking results indicate that the compound has been formulated to withstand the specified accelerated exposure without visible damage.
4. Typical Technical Data
The following table summarizes the principal performance data supplied for the five listed grades. The values are typical reference values rather than a substitute for a formal certificate of compliance, production specification, or project-specific qualification.
| No. | Test item | Unit or condition | Standard | DS-WDZH-01 | DS-WDZH-02 | DS-WDZH-03 | DS-WDZH-B1 | DS-WDZH-B2 |
|---|---|---|---|---|---|---|---|---|
| 1 | Density | g/cm³ | Not specified | 1.48 | 1.49 | 1.50 | 1.57 | 1.55 |
| 2 | Tensile strength | MPa | 10.0 | 12.0 | 12.0 | 12.5 | 11.2 | 11.2 |
| 3 | Elongation at break | % | 160 | 180 | 180 | 180 | 170 | 170 |
| 4 | Tensile-strength change after heat aging | % | ±25 | +10 | +12 | +9 | +12 | +14 |
| 5 | Elongation change after heat aging | % | ±25 | -5 | -10 | -12 | -15 | -12 |
| 6 | Hot deformation at 90°C for 1 hour | % | ≤50 | 10 | 10 | 8 | 5 | 5 |
| 7 | Embrittlement temperature by impact | °C | -25 | -25 | -25 | -25 | -25 | -25 |
| 8 | Volume resistivity at 20°C | Ω·cm | ≥1012 | 1.5×10¹³ | 1.5×10¹³ | 1.2×10¹³ | 2.5×10¹³ | 2.5×10¹³ |
| 9 | Smoke density, non-flaming | Test value | ≤350 | 305 | 320 | 340 | 260 | 280 |
| 10 | Smoke density, flaming | Test value | ≤100 | 70 | 70 | 65 | 50 | 55 |
| 11 | Oxygen index | % | ≥30 | ≥35 | ≥32 | ≥30 | ≥40 | ≥38 |
| 12 | Halogen acid gas content | % | ≤0.5 | <0.5 | <0.5 | <0.5 | <0.5 | <0.5 |
| 13 | pH value | Test value | ≥4.3 | 5.2 | 5.1 | 5.3 | 5.5 | 5.5 |
| 14 | Conductivity | μS/mm | ≤10 | 1.1 | 1.1 | 1.1 | 1.2 | 1.2 |
| 15 | Heat resistance to shock at 130°C for 1 hour | Visual result | No cracking | No cracking | No cracking | No cracking | No cracking | No cracking |
| 16 | Ozone resistance at 25°C for 24 hours and 300 ppm | Visual result | No cracking | No cracking | No cracking | No cracking | No cracking | No cracking |
The data show that the grades are not identical formulations with only a different product label. They offer different balances of density, flame performance, smoke generation, mechanical properties, and electrical insulation. The B1 and B2 grades generally provide stronger smoke and oxygen-index performance, while the general-purpose grades provide high elongation and tensile strength. This range allows cable manufacturers to select a compound according to the actual performance priority of each cable design.
5. Advantages Over Conventional and Lower-Specification Alternatives
5.1 Compared with Halogen-Containing Sheathing Materials
The most direct advantage is the product’s halogen-free and low-corrosivity combustion profile. Conventional halogen-containing sheaths may produce acidic gases and dense smoke when exposed to fire. The reported acid gas, pH, conductivity, and smoke results demonstrate that these LSZH grades are designed to reduce those risks.
This can be particularly valuable for projects where post-fire equipment damage is a major concern. A cable fire may affect more than the cable itself. Corrosive gases can travel through ventilation paths and settle on electrical equipment far from the original ignition point. By reducing halogen acid gas generation, an LSZH cable system can help limit this form of secondary damage, subject to the complete cable design and installation environment.
5.2 Compared with Low-Cost Flame-Retardant Compounds
Some lower-cost flame-retardant compounds achieve basic flame resistance by using high filler levels or additive packages that compromise flexibility, elongation, process stability, or low-temperature behavior. The material described here is positioned as a more balanced solution. It combines oxygen-index performance with elongation values of 170 to 180 percent for most grades, low hot deformation, low-temperature impact resistance, and resistance to heat shock and ozone cracking.
This balance can lower the risk of failures during cable production and installation. A compound that is excessively stiff or brittle may require more careful handling and may be more vulnerable to damage at bends, terminations, and pulling points. The reported mechanical properties support a more robust processing and service profile.
5.3 Compared with Generic Thermoplastic Sheaths
Generic thermoplastic sheath materials may provide good processing performance but lack the specialized combination of low smoke, zero halogen, flame retardancy, and low corrosivity required for modern power infrastructure. The present grades are formulated specifically for cable applications where fire performance and electrical protection must work together.
The product also provides a choice of grades. A manufacturer does not need to use the same formulation for every application. General grades can be selected for standard LSZH requirements, while B1 and B2 grades can be considered for projects with more demanding smoke or flame-retardant expectations.
5.4 Compared with Formulations Focused Only on Indoor Fire Safety
Some materials are designed primarily for indoor fire safety and may not have adequate outdoor durability. The listed resistance to ultraviolet exposure, moisture, mold, ozone, heat shock, and cracking indicates that these grades are intended for a broader range of cable environments. This is important for power grid systems, where the same project may include outdoor runs, buried sections, switchgear connections, and enclosed cable routes.
A compound that supports both indoor and outdoor cable applications can simplify material selection and qualification. It may also help cable manufacturers maintain a consistent product platform while adapting the grade to the required fire performance.
6. Advanced Manufacturing and Research Strengths
The development of a high-performance LSZH compound requires more than the selection of a flame-retardant additive. It involves polymer design, additive compatibility, compounding control, extrusion behavior, cross-linking performance, testing, and application feedback. The manufacturer described in the supplied information operates in the field of polyolefin cable compounds and maintains dedicated research, production, and testing capabilities.
Its research and development center covers more than 3,000 square meters and is equipped with research equipment valued at more than RMB 35 million. The organization includes a professional research and development team of more than 30 members, including five doctors and personnel recognized through provincial and municipal talent programs. This structure provides a technical foundation for formulation design, process optimization, performance testing, and customer-specific development.
The company operates two production bases covering more than 15,000 square meters and has more than 10 production lines for polyolefin cable compounds. Such production capacity is important for customers that require stable supply, repeatable quality, and the ability to scale from qualification samples to regular commercial orders.
6.1 Polymer and Additive Integration
LSZH materials must maintain compatibility among the polymer matrix, mineral flame-retardant components, stabilizers, processing aids, pigments, and other functional additives. Poor dispersion can create weak points, surface defects, inconsistent flame performance, or unstable electrical properties. A capable compounding operation must therefore control feeding, mixing, melt temperature, residence time, cooling, pelletizing, and packaging.
The manufacturer’s specialization in polyolefin cable compounds supports an application-oriented approach to these challenges. Rather than treating the material as a general-purpose plastic, the development process can be organized around cable extrusion behavior, sheath performance, cross-linking requirements, electrical insulation, and long-term environmental exposure.
6.2 Production Line and Process Control
Multiple production lines provide flexibility for different grades and customer requirements. They can support production planning, material segregation, process optimization, and capacity management. In a technical cable compound, consistency from batch to batch is essential. Small changes in filler distribution, moisture, additive concentration, or melt processing can influence extrusion pressure, surface appearance, mechanical properties, and fire performance.
Professional production control should include incoming raw-material inspection, controlled storage, accurate weighing and feeding, compounding parameter monitoring, pellet quality checks, packaging control, and retained-sample management. The supplied company profile emphasizes stable supply capacity and technical documentation, both of which are valuable for cable manufacturers operating under qualification and traceability requirements.
6.3 Testing and Application Support
Material selection should be supported by testing at several stages. Raw pellets can be examined for density, moisture, melt behavior, and basic mechanical properties. Extruded specimens can be tested for tensile strength, elongation, heat aging, hot deformation, electrical resistivity, smoke density, oxygen index, acid gas content, pH, conductivity, heat shock, and ozone resistance.
Finished cable testing is equally important. The same compound may behave differently depending on sheath thickness, conductor temperature, extrusion equipment, cross-linking procedure, cable geometry, and cooling method. Application support helps the cable manufacturer convert a promising laboratory formulation into a stable commercial process.
The company states that it provides application-oriented solutions, research and development support, testing support, technical documentation, stable supply, and customized material solutions. These capabilities can reduce the time needed to move from initial inquiry to validated cable production, especially when the customer requires a particular B1 or B2 performance profile, color, processing window, or environmental property.
6.4 Broad Product Development Experience
The product portfolio includes UV-crosslinked, silane cross-linkable, irradiation cross-linked, and thermoplastic low-smoke halogen-free flame-retardant cable compounds, as well as polyethylene sheath compounds and other specialized materials. This breadth is relevant because cable manufacturers often need multiple materials across one product family.
A supplier with experience in several cross-linking technologies can better understand the interactions between compound design and cable processing. It may also help customers coordinate conductor insulation, bedding, shielding, and sheath systems rather than selecting each compound independently.
7. Manufacturing Process Considerations for Cable Producers
7.1 Storage and Material Handling
LSZH compounds should be stored in clean, dry conditions and protected from moisture, contamination, and direct environmental exposure. Moisture can influence extrusion stability, surface appearance, electrical performance, and processing torque. Packaging should remain sealed until the material is ready for use, and opened bags should be managed according to the supplier’s processing guidance.
Different grades should be clearly identified and segregated. This is especially important when general LSZH grades and B1 or B2 grades are produced at the same facility. Traceability from raw materials to finished pellets and from pellets to cable batches supports quality assurance and simplifies investigation if a production deviation occurs.
7.2 Extrusion Optimization
The correct extrusion temperature profile depends on the grade, screw design, die geometry, line speed, cable construction, and equipment configuration. Excessive temperature can cause premature degradation or surface defects, while insufficient temperature may produce poor dispersion and unstable flow. The optimal process window should be established through controlled trials.
Key parameters may include feed-zone temperature, compression-zone temperature, metering-zone temperature, head temperature, die temperature, screw speed, extrusion pressure, line speed, cooling-water temperature, and take-up tension. A stable process should produce a smooth sheath with uniform wall thickness, acceptable surface finish, and no visible porosity, cracking, or contamination.
7.3 Cross-Linking and Final Performance
The supplied performance note states that the listed indicators apply after cross-linking. The cross-linking method and conditions should therefore be treated as part of the product system. Insufficient cross-linking may reduce heat resistance or dimensional stability, while excessive or uneven cross-linking may affect flexibility and process efficiency.
Manufacturers should validate the relationship between compound batch, extrusion conditions, cross-linking conditions, and final cable properties. A production qualification program should include testing of samples from the beginning, middle, and end of a run to confirm consistency.
7.4 Quality Control at Finished Cable Level
Finished cables should be checked for dimensions, surface appearance, tensile strength, elongation, heat aging, insulation resistance, sheath integrity, flame performance, smoke performance, and other project-specific requirements. Electrical tests may include conductor resistance, voltage withstand, insulation resistance, and water-related tests where applicable.
Because fire performance is influenced by cable construction, material testing alone cannot replace finished-cable qualification. The compound provides the foundation, but the complete cable must meet the applicable technical specification and installation requirement.
8. Application Areas
8.1 Transmission and Distribution Cables
Power transmission and distribution cables require a durable sheath that protects the internal electrical system from mechanical and environmental stress. The LSZH compound’s tensile properties, elongation, hot deformation performance, heat aging stability, and electrical resistivity make it suitable for consideration in these systems.
8.2 Buried Distribution Cables
Buried cables may be exposed to soil moisture, temperature changes, mechanical pressure, microorganisms, and installation tension. The material’s resistance to moisture, mold, cracking, and environmental aging supports its use in buried distribution applications, subject to the cable design and required water-blocking or mechanical protection systems.
8.3 Switchgear Wires and Equipment Connections
Switchgear rooms and electrical equipment areas can contain dense cable arrangements in enclosed spaces. Low smoke and low-corrosivity combustion behavior are valuable in these locations. The material can be considered for switchgear wires and related cable assemblies where a halogen-free flame-retardant sheath is required.
8.4 Outdoor and Overhead Cable-Related Applications
Outdoor cables are exposed to ultraviolet radiation, rain, humidity, ozone, wind, and temperature cycling. The product is described as resistant to ultraviolet exposure, moisture, mold, and cracking, and the test data show no cracking after the specified ozone and heat-shock tests. These characteristics support its consideration for outdoor cable applications.
8.5 Industrial and Infrastructure Projects
Factories, renewable energy installations, rail-related infrastructure, marine cable systems, new energy facilities, and communications projects often require specialized cable compounds. The manufacturer’s broader product portfolio and technical support capability may enable material selection across several cable types, including power, communication, photovoltaic, locomotive, marine, and rail transit applications.
9. Selecting Between the Available Grades
Grade selection should begin with the project’s required fire classification and cable construction. DS-WDZH-B1 and DS-WDZH-B2 show the highest typical oxygen-index values and lower typical smoke-density values in the supplied data. They may therefore be considered where enhanced flame and smoke performance is prioritized.
DS-WDZH-01, DS-WDZH-02, and DS-WDZH-03 provide typical tensile strengths from 12.0 to 12.5 MPa and elongation values of 180 percent. These grades may be attractive where high mechanical performance and flexibility are central to the cable design.
Density may also influence material consumption and cable weight. The general grades have reported densities of 1.48 to 1.50 grams per cubic centimeter, while the B1 and B2 grades show 1.57 and 1.55 grams per cubic centimeter. Cable manufacturers should consider sheath thickness, total cable weight, installation requirements, and transportation costs when choosing a grade.
No grade should be selected solely by one data point. A complete evaluation should consider flame performance, smoke density, mechanical properties, processing behavior, heat aging, low-temperature performance, electrical insulation, outdoor durability, regulatory requirements, and total project cost.
10. Environmental and Regulatory Considerations
The product information identifies compliance or alignment with environmental requirements such as GB/T 32129-2015, RoHS 2.0, and REACH. These references are relevant to customers seeking cable compounds that support environmental management and restrictions on hazardous substances.
Regulatory requirements can vary according to the country, market, cable type, project owner, and final application. Cable manufacturers should obtain current declarations, test reports, safety documentation, and compliance statements before using the material in a regulated project. The compound’s environmental status should be evaluated together with pigments, processing aids, cross-linking agents, and other components used in the final cable.
From a sustainability perspective, lower smoke and reduced corrosivity can help limit the consequences of fire, while material consistency and long service life can reduce premature cable replacement. Responsible material selection also includes efficient processing, minimized production waste, proper handling of off-specification material, and appropriate end-of-life management.
11. Quality Assurance and Customer Service
For cable compound customers, product quality includes more than laboratory performance. It also includes batch consistency, delivery reliability, documentation, technical communication, and responsiveness during production qualification. The manufacturer’s stated focus on stable supply, testing support, technical documents, and customized solutions addresses these practical requirements.
Technical documentation should normally include a product data sheet, recommended processing guidance, safety information, compliance declarations, packaging information, storage recommendations, and available test reports. Customers may also require batch certificates, sample retention, change-notification procedures, and technical support during extrusion trials.
A strong supplier relationship is particularly useful when a cable manufacturer needs to customize color, density, hardness, flame performance, extrusion behavior, or environmental resistance. Customization should be supported by a controlled development process with documented targets, sample approval, pilot production, and final validation.
The company’s location in Nantong, Jiangsu Province, places its production and research operations within one of China’s established industrial regions. Its two production bases and multiple production lines are intended to support both development and commercial supply. Customers should confirm current capacity, lead time, minimum order quantity, packaging options, and export documentation for each project.
12. Recommended Evaluation Procedure
A structured evaluation can help customers determine whether the material is appropriate for a specific cable.
Step 1: Define the cable requirement
Identify the conductor type, insulation system, sheath thickness, installation environment, operating temperature, minimum installation temperature, expected mechanical stress, fire classification, smoke requirement, environmental exposure, and applicable standards.
Step 2: Select candidate grades
Compare the standard LSZH grades with the B1 and B2 grades. Give priority to higher oxygen-index and lower smoke values when fire performance is the main requirement. Give priority to tensile strength and elongation when installation flexibility and mechanical handling are critical.
Step 3: Conduct laboratory processing trials
Process the material on the intended extrusion equipment. Record melt temperature, pressure, screw speed, line speed, die dimensions, cooling conditions, surface appearance, and dimensional stability. Confirm that the compound has a workable processing window.
Step 4: Produce pilot cable
Extrude the compound onto the actual cable construction. Evaluate sheath concentricity, wall thickness, adhesion where relevant, surface finish, stripping behavior, bend performance, and compatibility with adjacent layers.
Step 5: Test the finished cable
Perform mechanical, thermal, electrical, fire, smoke, environmental, and aging tests required by the project. Test samples should represent the intended production process rather than only laboratory plaques.
Step 6: Approve the production specification
After successful qualification, establish the approved grade, processing window, inspection plan, packaging requirement, batch acceptance criteria, and change-control procedure. This creates a repeatable basis for commercial production.
13. Frequently Asked Questions
What is an LSZH cable sheathing compound?
An LSZH cable sheathing compound is a material formulated to produce low smoke and minimal halogen acid gas during combustion. It is used as an outer protective layer for cables where fire safety, reduced corrosivity, and environmental performance are important.
What is the main application of this product?
The product is designed for the outer protection of transmission and distribution cables. It is also compatible with buried distribution cables, overhead cable-related applications, switchgear wires, and other cable systems requiring thermoplastic LSZH performance.
What is the difference between the B1 and B2 grades?
B1 and B2 are product grades with enhanced flame-retardant positioning. In the supplied typical data, B1 has an oxygen index of at least 40 percent and a flaming smoke-density value of 50, while B2 has an oxygen index of at least 38 percent and a flaming smoke-density value of 55. The exact selection should be based on the applicable project classification and finished-cable test results.
Are the materials halogen-free?
The product is described as halogen-free, and the reported halogen acid gas content is less than 0.5 percent for every listed grade. Customers should review the current compliance documentation for the specific grade and final cable construction.
Do these compounds generate low smoke?
Yes. The reported non-flaming smoke-density values range from 260 to 340, while flaming values range from 50 to 70. All are within the supplied standard limits of 350 for non-flaming conditions and 100 for flaming conditions.
Can the material be used outdoors?
The product is described as resistant to ultraviolet exposure, moisture, mold, and cracking. The supplied data also show no cracking after the specified heat-shock and ozone-resistance tests. Outdoor suitability should nevertheless be confirmed for the complete cable, including its installation method and mechanical protection.
Can the material be used for buried cables?
Yes, it is identified as compatible with buried distribution cables. The complete buried-cable design should also address water penetration, soil pressure, mechanical protection, temperature, and local installation requirements.
What is the tensile strength of the material?
The stated standard is 10.0 MPa. Typical values range from 11.2 to 12.5 MPa across the five listed grades.
What is the elongation at break?
The standard requires at least 160 percent. Typical values are 180 percent for DS-WDZH-01, DS-WDZH-02, and DS-WDZH-03, and 170 percent for DS-WDZH-B1 and DS-WDZH-B2.
Does the material resist heat?
The material shows controlled changes after air heat aging at 110 degrees Celsius for 168 hours. It also shows hot deformation values of 5 to 10 percent at 90 degrees Celsius for one hour and no cracking in the specified 130-degree-Celsius heat-shock test.
Is the material suitable for low-temperature installation?
All listed grades have a reported embrittlement temperature by impact of minus 25 degrees Celsius. The applicable minimum installation temperature should still be confirmed for the complete cable and project conditions.
What electrical insulation performance is reported?
Volume resistivity at 20 degrees Celsius is specified as at least 1012 ohm-centimeters. Typical values range from 1.2×10¹³ to 2.5×10¹³ ohm-centimeters.
Is the material thermoplastic or cross-linked?
The product category is thermoplastic LSZH sheathing compound. The supplied technical note states that the listed performance indicators are measured after cross-linking. Customers should confirm the required processing and cross-linking conditions for their specific cable design.
Can the grades be customized?
The manufacturer states that it provides customized material solutions. Customization may involve performance balance, processing behavior, color, or application requirements. Any customized grade should be validated through documented testing and cable qualification.
What support can a cable manufacturer expect?
The stated support includes application-oriented solutions, research and development assistance, testing support, technical documentation, stable supply capacity, and customized material development. Specific services, sample availability, delivery schedules, and documentation should be confirmed during technical discussions.
14. Conclusion
The LSZH flame-retardant sheathing material for power grids provides a comprehensive solution for cable manufacturers seeking low smoke, halogen-free combustion behavior, flame retardancy, mechanical durability, electrical insulation, and environmental resistance. Its five available grades allow engineers to balance general LSZH performance with enhanced B1 and B2 fire-related characteristics.
The reported data show tensile strengths of 11.2 to 12.5 MPa, elongation values of 170 to 180 percent for the listed typical values, low hot deformation, stable heat-aging behavior, volume resistivity up to 2.5×10¹³ ohm-centimeters, oxygen-index values of at least 30 percent, low halogen acid gas content, low conductivity, and no cracking after the specified heat-shock and ozone tests.
These properties provide advantages over conventional halogen-containing materials, generic thermoplastic sheaths, and lower-specification flame-retardant compounds. The value of the product lies in its balanced performance rather than in a single headline specification. It is designed to help protect cables during service while reducing the smoke and corrosive gas hazards associated with fire.
The manufacturer’s research center, professional technical team, multiple production bases, more than 10 production lines, broad polyolefin compound portfolio, and application-oriented support further strengthen the product’s commercial and technical position. For cable manufacturers, this combination of material performance, process knowledge, production capacity, and technical service can simplify qualification and support reliable long-term supply.
Before commercial adoption, each customer should confirm the appropriate grade through extrusion trials, cross-linking evaluation, finished-cable testing, regulatory review, and project-specific qualification. When these steps are completed, the material can serve as a strong foundation for safer and more durable power transmission and distribution cable systems.
References
1. Product technical data for DS-WDZH LSZH flame-retardant sheathing compounds, including DS-WDZH-01, DS-WDZH-02, DS-WDZH-03, DS-WDZH-B1, and DS-WDZH-B2.
2. GB/T 32129-2015, referenced environmental and performance requirements for cable materials.
3. RoHS 2.0, restrictions on hazardous substances in electrical and electronic equipment.
4. REACH, registration, evaluation, authorization, and restriction framework for chemical substances.
5. General technical principles for low-smoke, halogen-free cable compounds and finished cable evaluation.
6. Manufacturer-provided company profile and technical information concerning research, production, testing, and customized polyolefin cable compound solutions.